What the contact pin does in a fibre laser head
A sensor contact pin is the small conductive point that closes the sensing circuit used by the cutting head and ceramic assembly. In normal use it carries the machine signal from the head body into the height sensing system, so the control can read the sheet surface and keep the nozzle at the right distance during cutting.
On many fibre laser heads the pin sits inside a ceramic or insulated carrier, with the tip making repeatable contact against the mating surface. If the pin is worn, bent, heat stained or loose in its seat, the machine may hunt for height, lose a clean reference point, or leave poor edge quality on thin and medium sheet.
Pin styles, sizes and fit patterns
Contact pins are not one-size-fits-all. The working length, shoulder detail, thread pattern and tip shape must match the head design and the ceramic assembly around it. Some heads use a straight pin, others use a spring-loaded arrangement, and the interface can change between models even when the outside look seems close.
- Thread patterns commonly used in laser head assemblies, such as M2.5, M3 and M4.
- Short, medium and extended body lengths to suit different ceramic stack heights.
- Rounded, flat or fine-point contact tips, depending on the sensing face.
- Insulated or conductive body sections where the head layout calls for it.
- Matched seating shoulder for stable alignment inside the ceramic ring or carrier.
When the pin sits too proud it can wear the contact face too fast. If it sits too deep, the sensing path may be inconsistent and the head can lose repeatability at the start of a cut.
Where this part suits in sheet-metal production
These pins suit fibre laser cutting heads used on sheet-metal machines in general fabrication, cabinet work, HVAC ducting, signage and service centres that cut mild steel, stainless steel and aluminium. They are especially useful where the machine relies on capacitive height sensing and the operator wants a stable reference between the nozzle, ceramic stack and sheet surface.
In busy shops around Spartan, East Rand, Johannesburg, Pretoria, Durban, Cape Town and Rustenburg, the same pin can see repeated starts, stop-start nesting, mixed sheet thicknesses and frequent nozzle checks. Those conditions are hard on small sensing parts, and a worn pin can show up as inconsistent height on corners or during restarts after a pierce.
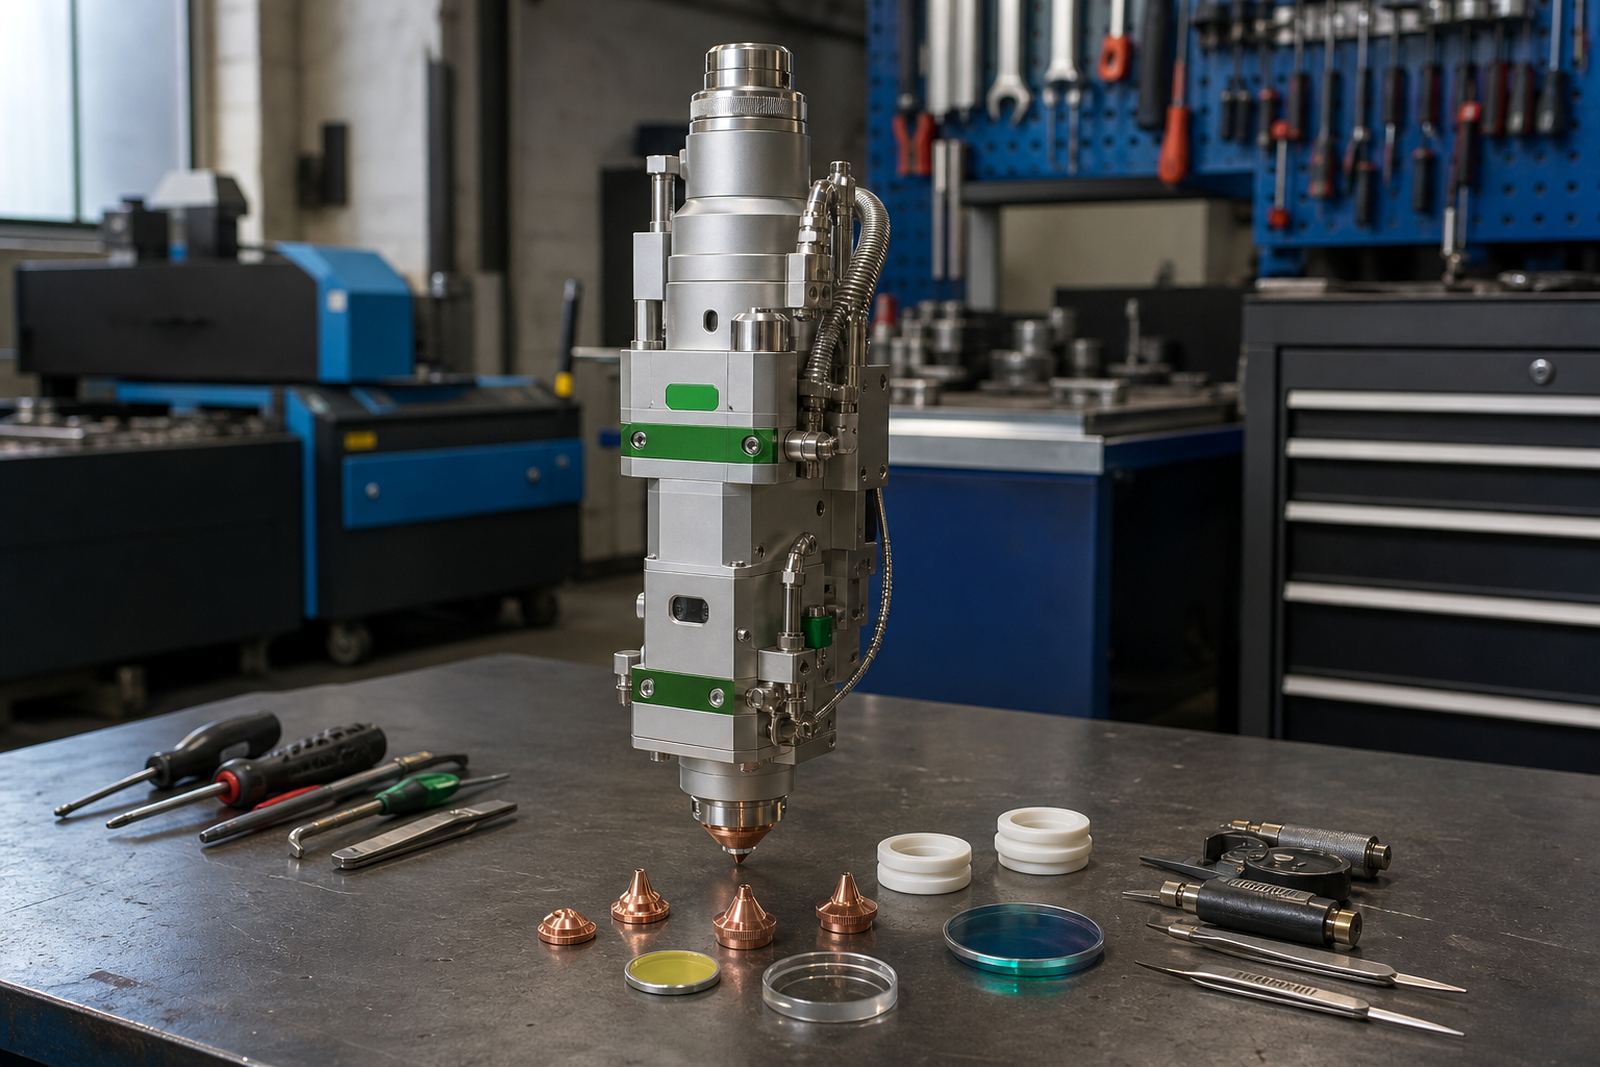
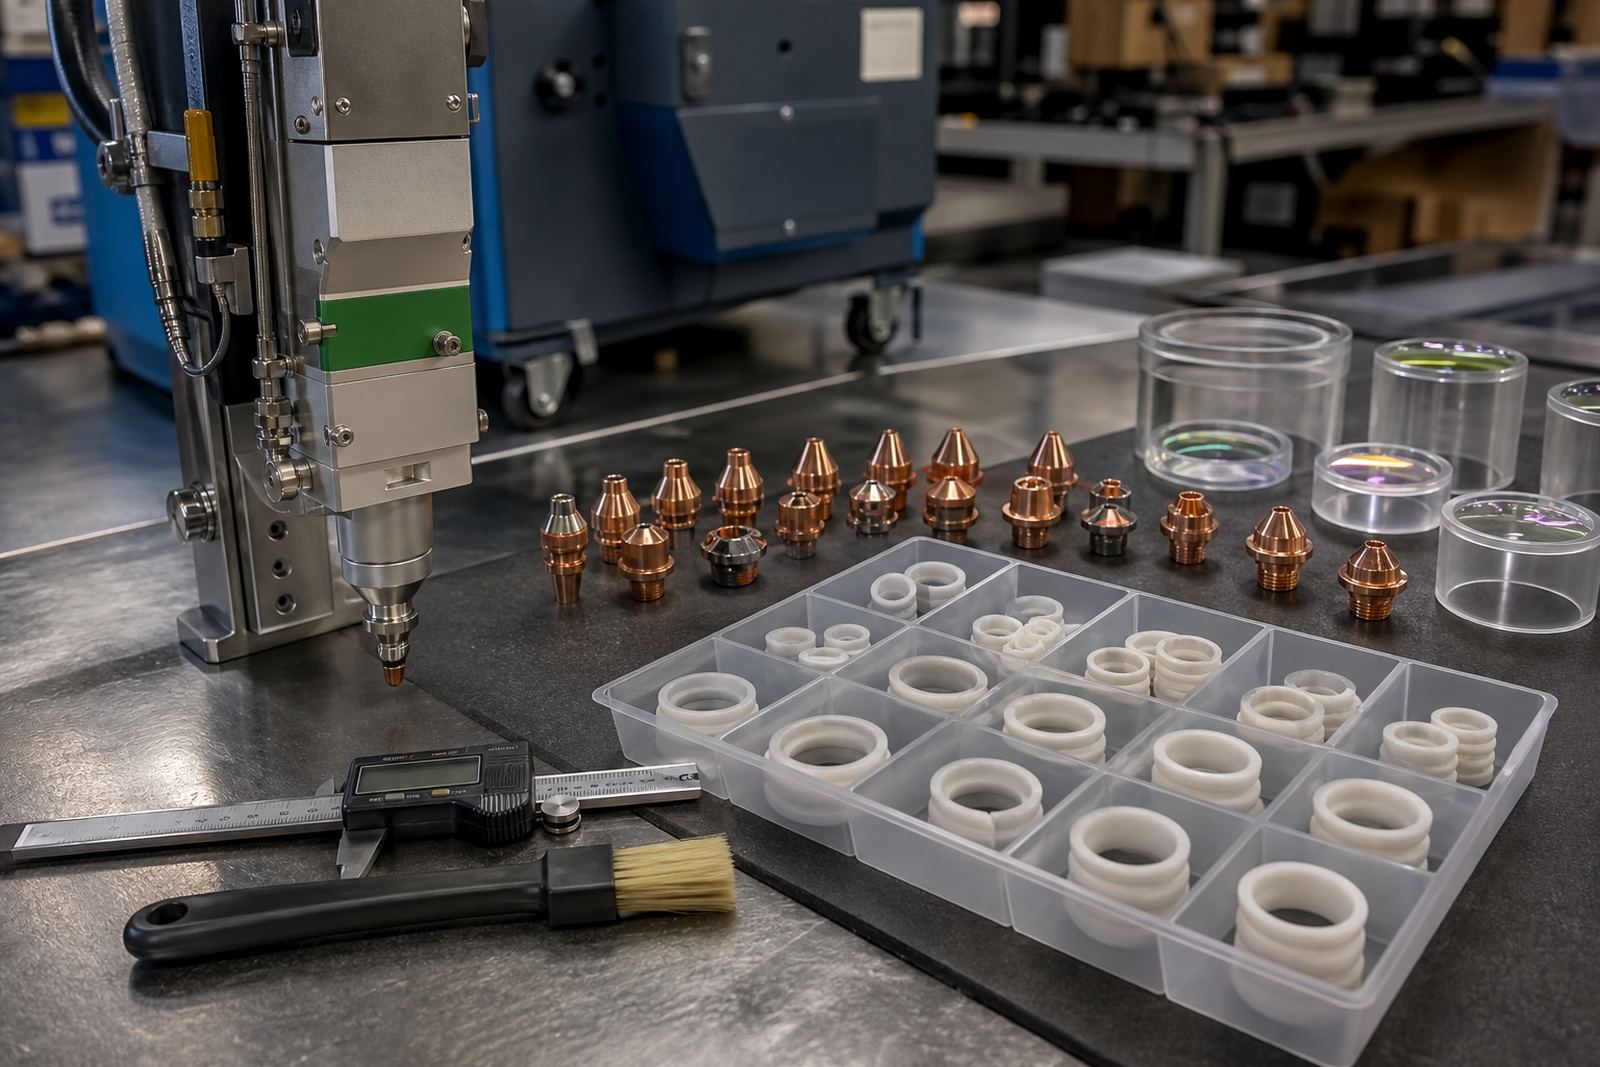
Our bench team also checks the surrounding parts when a pin is being replaced. Ceramic rings, nozzle centring, focus setting, lens condition and the gas path all affect the way the sensing circuit behaves at the head.
Fitting notes for a clean sensing path
Installing a sensor contact pin is a small job, but it needs care. The head should be isolated, the ceramic assembly kept clean and the mating faces checked for dust, slag fines and heat marks. A pin that is overtightened can pinch the ceramic stack or distort the contact path, while a pin left loose may chatter under vibration.
During fitment we check the pin seat, the alignment of the ceramic assembly and the stability of the contact face. If the head has taken a crash, the pin may not be the only part affected. A damaged ceramic ring, bent nozzle seat or disturbed focus position can all interfere with the sensing signal and call for more than a simple swap.
- Check the thread size before fitting.
- Match the pin length to the head stack height.
- Inspect the ceramic face for chips or carbon marks.
- Confirm the contact tip sits square to the mating surface.
- Test the sensing circuit after replacement and before production cutting.
Care, cleaning and wear signs to watch
Contact pins last longer when the head is kept clean and the ceramic area is free of dust, metallic fines and oil film. A light cleaning routine around the nozzle seat and sensor area helps the pin keep a stable electrical contact. If the machine runs stainless or aluminium often, fine residue can build up faster and the head needs a closer look.
Signs of wear include pitting on the tip, a dull or blackened contact surface, weak signal behaviour, intermittent height sensing or a pin that no longer seats properly after repeated cleaning. If the head has suffered a nozzle strike or a crash, the pin should be checked with the ceramic ring and the sensor path before the machine goes back into a shift.
For bench work and on-site head alignment, we also look at focus repeatability, nozzle centring and protective window condition because those parts can mask a sensing fault if they are out of line.
Details we need to check before ordering a replacement pin
To match the right contact pin to a fibre laser head, the main details are the head model, the ceramic assembly pattern and the thread form. The sensing style also matters, because some heads use a direct contact arrangement while others rely on a slightly different stacked layout inside the ceramic section.
Have the following details ready when you send the enquiry through our contact form: head model, thread size, overall pin length, tip profile, whether the head uses a spring-loaded pin, and whether the fitment is for bench service or on-site repair. If the head has already been stripped, a clear photo of the ceramic assembly and the old pin helps with the match.
Our Spartan, Kempton Park team supplies parts for sheet-metal shops that need the sensing path kept neat and repeatable, and we also fit related items such as protective windows, lenses, nozzles and ceramic rings when the full head service is being done.
Key facts
| Part type | Sensor contact pin for capacitive sensing in fibre laser cutting heads |
|---|---|
| Common thread patterns | M2.5, M3 and M4 depending on head design |
| Body styles | Straight, shoulder type and spring-loaded variants |
| Tip forms | Rounded, flat face and fine-point contact tips |
| Typical materials | Conductive metal body with insulated or ceramic-matched seating |
| Related fitment | Works with ceramic assembly, nozzle seat and sensing circuit alignment |